
Introduction: A Shop Floor Moment, Some Numbers, and a Question
I was standing next to a reflow oven watching tiny beads of solder smoke curl up like morning fog in a mercado. In many small factories, fume extraction for electronics and industrial applications is still an afterthought—yet studies show soldering fume exposure can exceed safe limits in under an hour for busy lines. (Sí, I mean real exposure numbers.) How do we fix this without killing throughput or blowing budgets? Let’s walk through what I’ve seen on shop floors and what the data quietly tells us next.
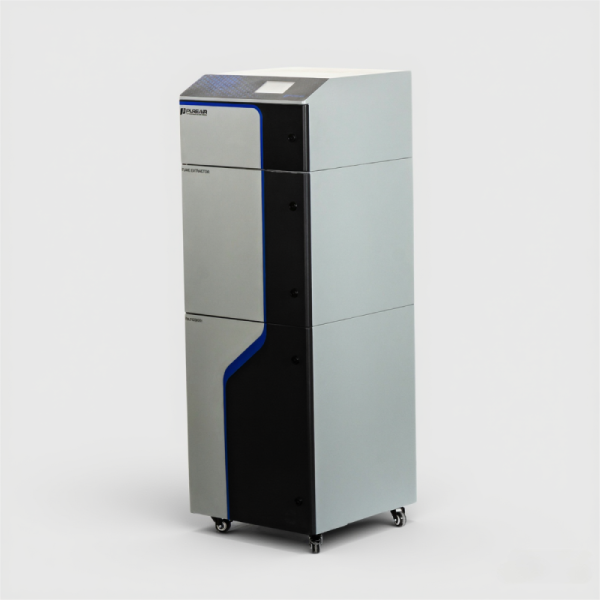
Why Classic Fixes Fall Short in Electronic Product Manufacturing
electronic product manufacturing often relies on band-aid solutions: window fans, point vacuums, or undersized HVAC tweaks. I’ve been in plants where extraction arms are set too far from the source, and HEPA filters are treated like wishful thinking. These fixes reduce visible smoke but miss fine particulates and volatile organic compounds (VOCs). The result? Operators still report headaches and managers see repeat QC failures. Look, it’s simpler than you think — placement, capture velocity, and filter choice matter more than loud promises.
Let’s get technical for a moment. Proper source capture requires a matched system: correct extraction arms, enough capture velocity at the soldering point, and filters rated for both particulate and gaseous phases. Many shops skip ambient sensors and assume one fan fits all. That causes uneven airflows and pockets of contamination. I’ve watched a factory add a central scrubber but ignore the duct layout — and the improvement was minimal. The lesson: system design is part physics, part practical work flow. Soldering fume, HEPA filters, and extraction arms are not optional—they’re the foundation.
Is the investment worth it?
Short answer: yes. Better capture reduces worker sick time, lowers rework, and protects reputations. But you must match technology to process. I’ll show why next.
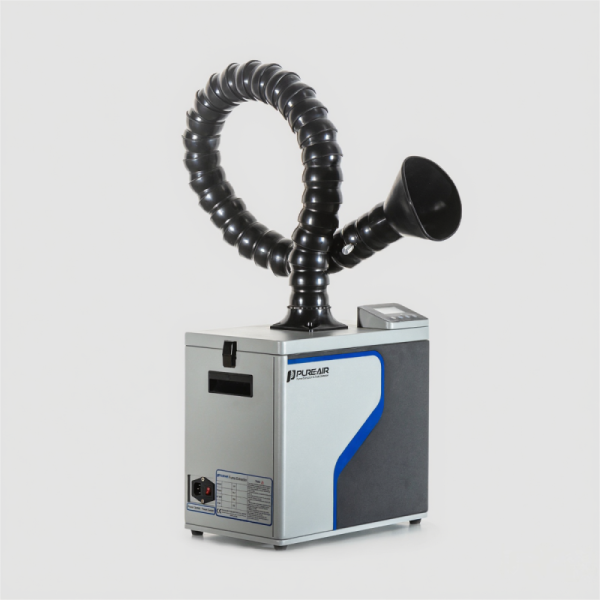
New Principles for Cleaner Processes and Future Outlook
Moving forward, I favor systems built on a few clear principles. First: capture at the source. Second: layered filtration that handles particulates and gases. Third: smart monitoring—ambient sensors plus basic data logging so you see trends, not just alarms. In electronic product manufacturing, that looks like compact extraction hoods at solder stations, an in-line HEPA plus activated carbon stage, and simple dashboards that show hours of exposure per station. Add edge computing nodes for local logging if you want advanced analytics, but you don’t need them to get big wins.
What about cost? I won’t lie—upfront spend is real. But when you factor lower absenteeism, fewer rejects, and better compliance, the payback is often faster than teams expect. — funny how that works, right? We should also plan for modular upgrades. Start with a proper hood and a rated filter bank. Then add ambient sensors and local controllers. Power converters for extraction fans should be steady and quiet; vibrations destroy seals and invite leaks. This staged approach keeps cash flow sane and lets you learn as you go.
What’s Next — Real-World Steps?
Here are three metrics I use when evaluating systems. First, capture efficiency at the source (measure with a vane or Pitot tube). Second, filter effectiveness for both particulate (e.g., MPPS) and gas-phase contaminants (activated carbon capacity). Third, measurable reduction in operator exposure over time—use simple badges or short-term sampling. These give you objective proof that a solution works. In practice, I recommend trials on a line for 30 days with baseline and follow-up sampling. That’s how you stop guessing and start improving.
Closing Guidance — How I Choose Systems
I’ll leave you with three practical evaluation points to guide decisions. 1) Does the design prioritize source capture over room dilution? 2) Are filters selected for both particulates and VOCs and easy to replace? 3) Is there simple monitoring that tells you when performance drops? If the answer is yes to all three, you’re on the right track. I’ve seen plants transform worker comfort and product quality by making those choices. If you want a real partner who understands small lines and big plants, check brands with proven solutions and local support — they matter. For example, PURE-AIR has system options that fit many of the steps above. I speak from experience when I say small changes can make a big difference — and they often pay back faster than you fear.