
Introduction: A Shop Floor Moment, Numbers, and a Question
I remember standing beside a machinist who sighed as a part sat idle while the turret did yet another slow tool change; he called it “wasted money.” Turret lathe manufacturers sit at the center of that pain — they decide how fast a shop moves, how accurate parts are, and ultimately how margins look. Recent shop-floor surveys I trust show small-to-mid shops losing roughly 8–15% of available time to setup and tool-change delays (and yes, that eats into quarterly forecasts). So, what do you do when your CNC control, turret indexing, or spindle strategy is the bottleneck — upgrade, retool, or change supplier? Let’s walk through why the choice of supplier matters and what it really buys you on the balance sheet; then we’ll dig deeper into the hard-to-see problems that vendors rarely warn you about.

Part 2 — Why Traditional Choices Fall Short (deeper layer)
turret milling machine supplier — I say this because I’ve seen shops chase low price and then pay more in downtime. Historically, suppliers sold turret designs that emphasized simple turret indexing and basic tooling capability. That works for single-run shops, sure, but once you scale batch sizes or add tighter tolerances, weaknesses show: tool chatter from an under-damped spindle, inaccurate turret repeatability, and control firmware that lags modern CNC control features. I don’t sugarcoat it — these are real cash drains. Look, it’s simpler than you think: better turret dynamics and tooling strategy can cut cycle time and scrap. In my experience the worst part is predictability is lost; you might hit a quality target one day and miss it the next because the chuck alignment shifts slightly or feed rate tuning wasn’t done right.
What specific flaws bite production teams?
First, many legacy turrets assume a constant feed rate profile; they don’t adapt to heavy cross-sections or hard spots in material. That leads to more heat, faster tool wear, and rework. Second, tooling ecosystems are sometimes locked to a vendor’s tool holders — so you get limited options for high-performance inserts. Third, maintenance cycles are manual and opaque: no live telemetry from bearings or turret indexing mechanisms, which means failures come as surprises. I’ve pushed teams to demand better data hooks — spindle sensors, servo diagnostics, and simpler retrofit paths for improved chuck and lathe bed stability. When suppliers won’t share cycle models or help tune feeds, that’s a red flag. — funny how that works, right?
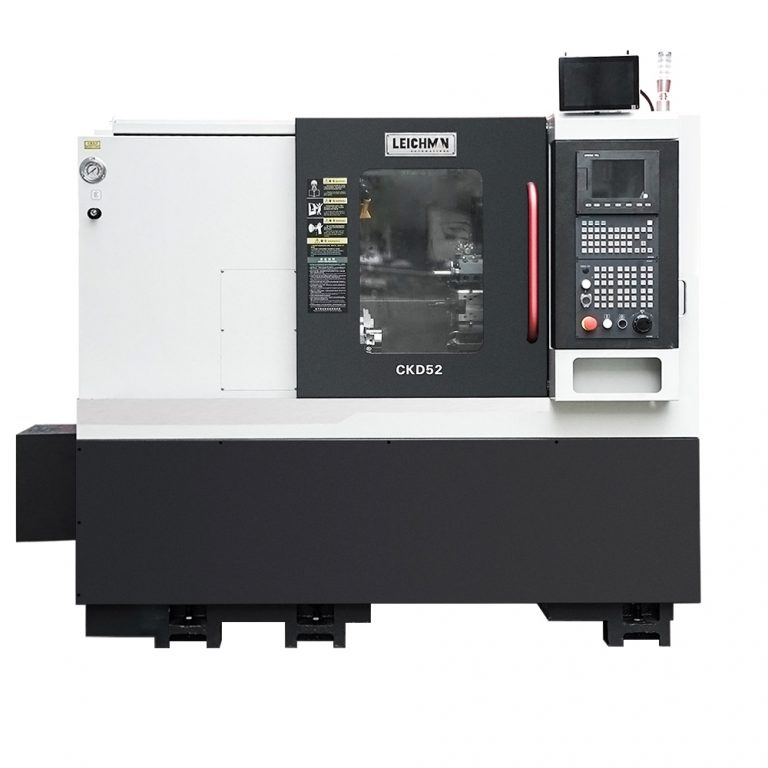
Part 3 — New Principles and a Forward View
Now, let’s look ahead with practical tech principles that matter for choosing vertical turret lathe manufacturers and futureproofing throughput. I focus on three technology shifts I want in every machine spec: integrated servo motor diagnostics, adaptive feed-rate logic in the CNC control, and modular tooling interfaces that accept third-party high-performance inserts. The point isn’t hype — it’s measurable: reduced cycle variance, longer tool life, and fewer emergency stops. I like to test suppliers on those principles in a short pilot run — 50 to 200 parts — and watch variability. If the numbers don’t improve, I move on.
What to measure next
Compare control logs for feed-rate adjustments, inspect spindle vibration signatures, and review turret indexing tolerance reports. These are not glamorous metrics, but they predict maintenance costs and part quality. For a future-oriented buy, also ask how a vendor supports remote diagnostics and firmware updates. Some suppliers design open telemetry hooks so you can push analytics later — a practical win if you’re building capacity without overhauling the floor. I’ve seen teams triple uptime after switching to platforms that prioritized these elements. — and yes, the initial cost was higher, but ROI came within a few months.
Closing — Three Practical Metrics I Recommend
We’ll end with three clear, business-minded evaluation metrics I use when vetting suppliers: 1) Cycle-time stability: measure variance across 100 parts, not just mean time. 2) Tooling flexibility: confirm support for third-party inserts and quick-change holders. 3) Diagnostics openness: require access to spindle and turret telemetry. Apply those and you’ll separate vendors who sell machines from those who enable predictable production. I’ll be blunt — I prefer partners who help me test on the floor and share real run data. If you want a starting point, look into the platforms and offerings from Leichman; they tend to align with these practical principles and have supported hands-on trials with my teams.