
Introduction — a shop-floor moment, some numbers, one big question
I remember standing over a tired VMC late one night, watching a part spit out with a chatter mark and thinking: there has to be a better way. Vertical machining center manufacturers get this call every week — shops complain about downtime, inconsistent finishes, and hidden costs that quietly add up. Recent surveys show a surprising fact: about 60% of small-to-mid shops report more scrap and setup time than they budget for (that’s real cash). So, how do you choose a machine that actually fits your workflow and budget without the constant headaches?
I write from hands-on experience and a lot of late shifts. I want to walk you through what I’ve learned, plainly and practically. We’ll look at the problems that trip teams up, the technical limits that matter, and what to ask suppliers. Stay with me — the next section peels back the old fixes that sound good on paper but fail on the floor.
Deep Dive: Why standard fixes fail (and what users quietly suffer)
Why do standard solutions break down?
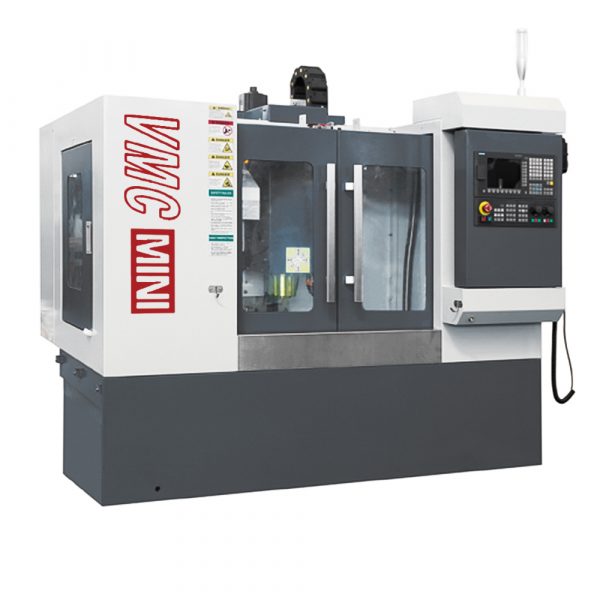
Let’s start technical — but in human terms. When somebody recommends a new control or faster spindle, they often mean well. Yet many shops find those upgrades don’t fix the root cause. A cnc vertical machining center will only deliver when the whole system is balanced: spindle speed, tool changer reliability, axis controller tuning, and coolant delivery must all work together. Too often, vendors sell one shiny part and leave you with integration headaches. I’ve seen this firsthand: a high-speed spindle bolted onto an old feed system simply moves problems elsewhere.
Hidden pain points are sneaky. Setup complexity costs time. Inconsistent tool changers add scrap. Poor servo drives tuning creates vibration that shows up as chatter on final surfaces. Look, it’s simpler than you think: you don’t always need the fastest spindle; you need the right mix of throughput, stability, and predictable maintenance. Users suffer from downtime they didn’t plan for, spare-parts pileups, and training gaps that nobody budgeted. I’m speaking plainly because I’ve sat through those shop-floor calls and helped people fix the real bottlenecks — not just the symptoms.
Looking Ahead: Future outlook and how suppliers fit in
What’s Next for your shop?
Now let’s move forward. I’m optimistic about practical improvements — not magic fixes. New principles focus on systems thinking: matched components, real-time diagnostics, and clearer operator interfaces. That means thinking about power converters that stabilize torque under load, or edge computing nodes that flag wear before it becomes a meltdown. When you evaluate a cnc vertical machining center supplier, look beyond specs and ask how they support integration, spare parts, and training.
Case example: a mid-size shop I worked with replaced a dozen erratic machines with two modern VMCs and reworked workflows. The payoff wasn’t just speed — it was fewer tool changes, less scrap, and predictable cycles. The supplier provided service training and parts kits. Result: uptime climbed, and the team felt confident again — funny how that works, right? I can’t promise every shop gets the same numbers, but the principle holds: matched systems and honest supplier support beat flashy numbers alone.
To wrap up, here are three quick metrics I use when advising teams: mean time between failures (MTBF), first-part accuracy over a 30-day run, and total cost of ownership including downtime. Use those to compare offers. I recommend starting conversations with suppliers about real shop scenarios, not hypothetical max rpm. If you want a partner that speaks plain and acts practical, consider talking to Leichman.