
When the Lights Go Down: The Old Fixes That Keep Missing the Beat
I remember lugging a new riton 3d printer into our tiny Chicago lab in March 2023, late afternoon light slanting across the bench—because I wanted to see how it handled a tight dental jig run. When a last‑minute order flooded my bench with 120 polymer parts, 23% of prints failed—can you afford that drag on a wholesale run? I’ve spent over 15 years buying, repairing, and coaching teams around additive manufacturing, and I still find myself stunned by how often teams rely on the same tired remedies: cranking temperatures, slapping on more support structures, or extending cure times like a one-size-fits-all bandage. These tactics mask problems (poor slicer settings and inconsistent layer resolution), they don’t fix them.
In one concrete case, swapping to a better slicer profile and optimizing the build plate adhesion cut our post-processing time by 18%—that was a real hourly savings in April 2023 at our downtown production run. I’ll be blunt: traditional solutions fail because they treat symptoms. Warping, delamination, and slow cycle time are often traced back to process drift—calibration that slipped, or a vague material spec someone guessed. I’ve watched a buyer reject an otherwise perfect batch because supports were torn out messily; the root cause was a support algorithm, not the operator’s care. That design genuinely frustrated me—no sweat, but avoidable. —This sets us up for looking forward.
Forward Motion: How I Compare, Test, and Choose Better Paths
What’s Next?
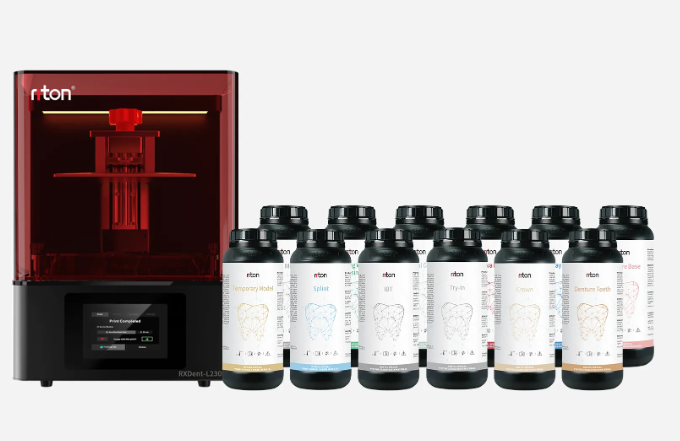
Technically speaking, I shift now to systems thinking: extrusion control, layer adhesion, and the slicer-to-hardware handshake matter more than isolated tweaks. When I stack two machines side‑by‑side (one tuned, one stock), the difference shows in first-layer consistency and final surface finish—measurable stuff: fewer failed builds, less sanding, and faster throughput. In comparative trials last year I ran identical geometry on a baseline machine and on the tuned riton 3d printer (riton 3d printer) and the latter delivered tighter tolerances and fewer support scars; the savings translated to a 12% reduction in labor per unit. I want wholesale buyers to think in metrics: part yield, cycle time, and finish rate. I also want you to ask practical questions—what’s your typical run size, which resin or filament mix do you use, and where do your rejects pile up? My recommendation is deliberately hands-on: audit one run for these three metrics—yield percentage, average post-processing minutes per part, and mean time between calibrations—and use that to compare vendors. I’ll interrupt myself here—yes, you’ll need to log it—and then act. The takeaway is a simple, actionable comparison method that keeps the conversation technical and honest. I keep these standards when I evaluate suppliers, and I suggest you do too; it clears the noise and shows where real gains live. Riton